Direct factory procurement of verified cosmetic actives, functional supplement formulations, precision wellness tools, and customized label substrates.
The international supply chain for raw materials has undergone a fundamental structural pivot. In modern B2B procurement, multinational cosmetics houses, pharmaceutical distributors, and direct-to-consumer (DTC) wellness brands no longer evaluate raw material suppliers purely on unit pricing. Instead, global purchasing directors prioritize batch-to-batch chemical purity, ISO 22716 / GMPC compliance, rigorous trace analytical documentation (COA, HPLC, GC-MS), and regulatory compliance (FDA registration, EU CPNP, REACH).
As a premier China Wholesale Raw Materials Manufacturer & Factory backed by over 30 years of integrated OEM/ODM contract manufacturing expertise, MYT Cosmetics Manufacturing bridges the gap between raw biological/chemical synthesis and market-ready personal care products. From high-potency cosmeceutical actives like stabilized 3-O-Ethyl Ascorbic Acid and multi-molecular weight Hyaluronic Acid to bio-fermented probiotic blends and sustainable packaging roll stock, our infrastructure is engineered to mitigate cross-border supply chain volatility while maximizing product efficacy.
Founded in 1990, our facility operates under international Good Manufacturing Practice (GMP) protocols, housing fully automated emulsification, compounding, encapsulation, and clean-fill production lines. We provide an integrated, turn-key B2B platform that spans molecular raw material sourcing, customized formula development, rigorous micro-challenge testing, and full-scale retail package integration.
Every batch of raw material undergoes rigorous chromatographic and spectroscopic testing. Utilizing High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Atomic Absorption Spectroscopy, our chemical engineers ensure active concentrations strictly match client Certificate of Analysis (COA) specifications with zero heavy metal or micro-contaminant tolerances.
Our production cleanrooms strictly adhere to ISO 14644-1 Class 7 (Class 100,000) air purity guidelines. Featuring HEPA-filtered positive pressure ventilation, automated micro-dosing mixing vessels, and UV sterilization tunnels, we guarantee maximum bio-stability for preservative-free and delicate active skincare formulations.
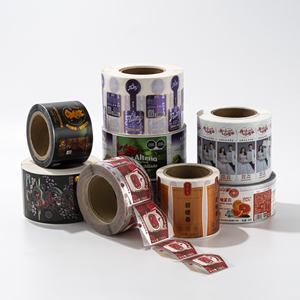
Beyond bulk liquid and chemical active synthesis, we provide complete, shelf-ready packaging manufacturing. Our facility handles industrial-grade custom adhesive vinyl printing roll stocks, glass bottle secondary packaging, eco-friendly aluminum tube sealing, and custom gift box assembly tailored for seamless global retail distribution.
Requirements & Technical Scope Definition
Custom Synthesis & Active Matching
Stability & Micro-Challenge Validation
Regulatory Dossier (MSDS/COA/PIF)
Automated GMPC Cleanroom Compounding
Cold-Chain & Freight Optimization
As consumer preferences shift rapidly toward transparency, clean label verification, and clinical efficacy, wholesale buyers must align their procurement strategies with upcoming regulatory shifts and bio-technological innovations. Industry data highlights 5 macro-trends governing raw material sourcing over the next decade:
Traditional chemical extraction is giving way to precision bio-fermentation. Actives such as bio-identical Ectoin, Ergothioneine, and Recombinant Humanized Collagen offer superior bio-compatibility, zero seasonal supply variation, and lower environmental footprints compared to conventional botanical harvesting.
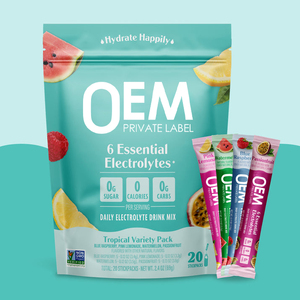
The boundary between topical cosmetics and oral supplements has dissolved. Brand owners are procuring functional nutraceutical ingredients—such as heat-stable probiotic strains, micro-encapsulated whey protein, and electrolyte premixes—to formulate complementary "In-and-Out" anti-aging beauty regimens.
Global regulations (such as EU packaging directives) strictly restrict non-recyclable composite laminates. Modern packaging roll stocks now utilize water-based coating barrier films, biodegradable vinyl adhesive stocks, and mono-material recyclable plastics engineered to withstand aggressive essential oils and volatile solvents.
Institutional buyers demand real-time verification of batch origin and carbon accounting. Advanced raw material factories are deploying digitally signed COAs and QR-code accessible analytical testing dossiers, giving procurement managers end-to-end auditability from raw synthesis to final shipment.
| Evaluation Parameter | Legacy Botanical Extraction | Conventional Synthetic Actives | MYT Bio-Fermented & Stabilized Actives |
|---|---|---|---|
| Batch Purity Consistency | Variable (Dependent on harvest season) | High (>95.0%) | Ultra-High (>99.2% via HPLC) |
| Heavy Metal & Contaminant Limits | Requires complex post-purification | Trace catalyst residuals possible | <1 ppm (Exceeds USP/EP Standards) |
| Thermal & Photolytic Stability | Low (Rapid active degradation) | Moderate | Optimized via Micro-Encapsulation |
| Regulatory Dossier Support | Basic MSDS | Standard COA | Full Dossier (COA, MSDS, CPNP, REACH, Stability Data) |
| Carbon Footprint / ESG Profile | High agricultural land use | Petrochemical feedstock dependent | Low-Carbon Fermentation & Upcycled Byproducts |
Formulating high-performance skincare and nutraceutical products requires navigating complex chemical interactions. Unstabilized active ingredients often suffer from rapid oxidation, discoloration, or phase separation when subjected to ambient storage conditions. Our factory research team specializes in advanced stabilization technologies that preserve active potency over a guaranteed 24-to-36-month shelf life.
L-Ascorbic Acid degrades rapidly in aqueous solutions. By combining water-soluble 3-O-Ethyl Ascorbic Acid with Ferulic Acid and Vitamin E (Tocopherol) inside a liposomal lipid carrier, our factory achieves over 98.5% active retention even after 12 weeks of accelerated thermal stability testing at 45°C.
Single-weight Hyaluronic Acid only hydrateth the skin surface. Our advanced raw material premixes combine ultra-low molecular weight HA (<10 kDa for deep dermal penetration), medium molecular weight HA (100–500 kDa for barrier repair), and high molecular weight HA (>1.5 MDa for surface film formation) into a single cohesive gel complex.
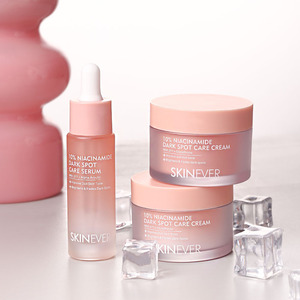
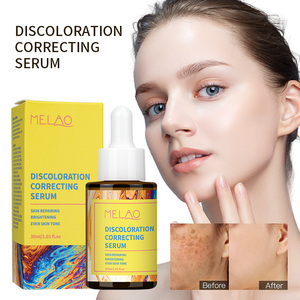
Low-grade Niacinamide raw materials contain trace residual Nicotinic Acid, which triggers skin flushing and irritation. MYT Cosmetics guarantees cosmetic-grade Niacinamide with Nicotinic Acid levels below 10 ppm, rendering our whitening creams and discoloration correction serums suitable for sensitive skin types.
Clear operational communication is vital for international contract manufacturing. Below are comprehensive answers to common technical and commercial queries raised by global purchasing directors:
Every production run is accompanied by a full compliance dossier including a batch-specific Certificate of Analysis (COA), Safety Data Sheet (SDS / MSDS) compliant with GHS standards, Product Information File (PIF), Stability Testing Reports, and Challenge Test (USP <51>) Results. For finished OEM cosmetics entering the European Union or United States, we provide technical support for CPNP portal notification and FDA VCRP registration.
For standard bulk active ingredients and established stock formulations (such as our core anti-aging serums or whitening creams), MOQs start at 500 units for packaged goods or 10 kg for bulk liquids. Custom molecular synthesis or specialized formula development requires an MOQ of 1,000 to 3,000 units depending on raw material rarity, container tooling requirements, and packaging customization specifications.
We operate in-house high-resolution flexographic and digital label printing machinery capable of producing waterproof vinyl adhesive sticker rolls, hot-foil stamped labels, and clear film substrates. Our automated labeling equipment ensures sub-millimeter precision application on bottles, jars, and soft chews packaging, eliminating label bubbling and alignment errors during high-speed bottling.
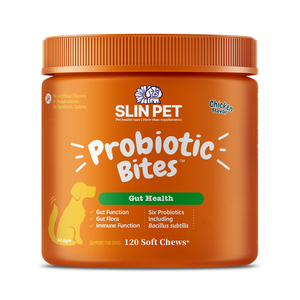
For nutraceutical products such as pet digestion soft chews and superfood electrolyte powders, we utilize micro-encapsulated spore-forming strains (e.g., Bacillus coagulans) combined with low-temperature cold-extrusion processing. This prevents thermal degradation during compression and ensures live CFU counts remain fully stable throughout the product's entire declared shelf life.
Initial R&D formula matching and sample dispatch typically take 3 to 7 business days. Upon sample approval and packaging artwork sign-off, bulk compounding and automated cleanroom filling are completed within 15 to 25 days. International shipping lead times vary by Incoterm (FOB, CIF, DDP), with express air freight requiring 5–7 days and sea freight shipping taking 20–35 days depending on destination port.
Accelerate your brand's market expansion with certified chemical purity, validated active stability, and seamless full-service contract manufacturing. Download our comprehensive product catalog or request custom formula samples today.
Get Catalog