Explore our GMP-manufactured wholesale airless bottle configurations. Designed for zero oxygen exposure, micro-dosing accuracy, and high formula evacuation rates.
 High Viscosity
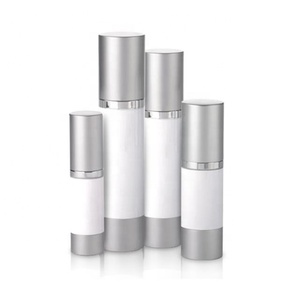 Luxury Series
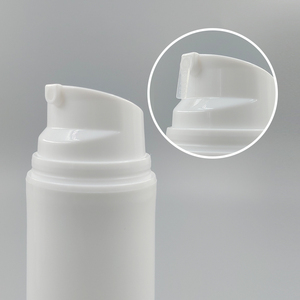 Mono-Material
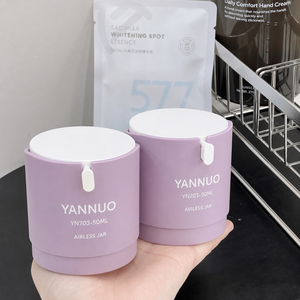 Airless Jar
 Travel Precision
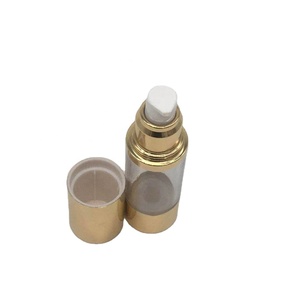 Crystal Clarity
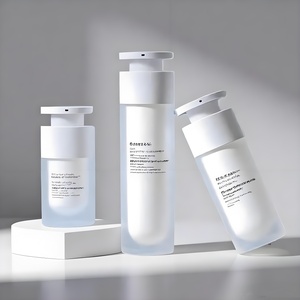 Double Wall
 PCR Customizable
Traditional dip-tube pumps introduce atmospheric air into the bottle container to replace dispensed fluid. In contrast, modern airless packaging relies on a non-dip-tube differential vacuum engine that safeguards active botanical ingredients, L-Ascorbic Acid (Vitamin C), and Retinol from oxidation degradation.
As the user presses the actuator engine, a micro-vacuum pressure differential is created inside the hermetically sealed cylinder. A precision Polypropylene (PP) piston at the bottom ascends sequentially, displacing product upwards without drawing ambient oxygen into the reservoir chamber.
Our engineered airless pumps place the metallic tension spring outside the liquid chamber. This eliminates trace heavy-metal leaching and ion interaction with acidic serums (pH 3.0–4.5), preventing formula discolouration, phase separation, or catalytic oxidation.
By engineering elastomeric check-valves and tailored nozzle orifices, our bottles dispense fluids ranging from low-viscosity liquid essences (500 cPs) to heavy dental paste formulations and cosmetic butter emulsions (120,000 cPs) with volumetric accuracy within ±0.015 ml.
Comparative laboratory testing reveals that premium anti-aging serums stored in standard dip-tube pump bottles lose up to 34% of their active Vitamin C concentration within 60 days of consumer unsealing due to continuous headspace oxidation. In MYT Cosmetics airless bottle packaging, the Oxygen Transmission Rate (OTR) is restricted to < 0.05 cm³/m²·day, retaining 97.2% active ingredient potency across a 24-month shelf life without synthetic chemical preservative loading.
A quantitative breakdown of packaging efficiency, formula protection, and procurement metrics for cosmetic brand purchasing managers and contract packaging engineers.
| Performance Specification | MYT Airless Pump Bottles | Standard Dip-Tube Bottles | Traditional Cosmetic Jars |
|---|---|---|---|
| Headspace Air Contact | 0% (Hermetically Sealed) | High (Air Re-enters per Pump) | 100% Constant Exposure |
| Product Evacuation Rate | 98.5% – 99.2% | 82.0% – 88.5% | 90.0% (Manual Scraping) |
| Preservative Need Level | Minimal / Organic Formulation | Standard Preservative System | Heavy Synthetic Load Required |
| Microbial Contamination Risk | Near Zero (Touchless) | Low-Medium | Extreme (Finger Contact) |
| Max Formulation Viscosity | 120,000 cPs (Pastes/Creams) | 15,000 cPs (Flowable Lotions) | Unlimited (Open Vessel) |
| Dosage Consistency Variance | ± 2.5% Volumetric Precision | ± 8.0% Volumetric Precision | Uncontrolled (Manual Dip) |
| PPWR Recyclability Grade | Class A (Mono-Material PP) | Class C (Multi-Material Dip Tube) | Class B/C |
Guided by over three decades of OEM & ODM packaging and contract manufacturing leadership, MYT Cosmetics operates fully integrated GMP-certified facilities serving top cosmetic brands across North America, Europe, Asia, and the Middle East.
Custom neck finishes, actuator caps, and bottle dimensions prototyped via 3D SLA modeling within 72 hours.
Selection of virgin food-grade PP/AS/PETG or certified Post-Consumer Recycled (PCR 25%–100%) resin blends.
Automated multi-color silk screening, hot-foil stamping, soft-touch spray coating, and custom electroplating.
Cleanroom high-speed assembly lines with optical sensor verification of piston insertion and torque tolerance.
As environmental regulations tighten and clean-beauty formulations evolve, the global wholesale airless bottle industry is undergoing rapid technical transformations. Staying ahead of these key sourcing trends ensures compliance and brand distinction.
Driven by the European Union Packaging and Packaging Waste Regulation (PPWR), traditional airless bottles featuring mixed plastics (e.g., SAN outer, PP inner, metal springs) are rapidly being replaced by 100% Polypropylene (PP) or Polyethylene (PE) mono-material packaging. These single-polymer systems can be directly dumped into domestic recycling streams without manual disassembly.
Eco-conscious luxury skincare brands are embracing dual-structure packaging: a durable, high-weight acrylic, glass, or aluminum outer sleeve combined with low-cost, lightweight replace-and-refill airless cartridges. Consumers retain the outer vessel indefinitely while purchasing sealed replacement pods, reducing brand resin consumption by over 70% per consumer cycle.
Airless technology is rapidly expanding beyond thin liquid facial serums into heavy oral hygiene pastes, dense body creams, hair masques, and medical ointments. Engineered heavy-duty spring mechanisms, widened pump stroke pistons, and non-clogging silicone flap valves enable reliable evacuation for formula viscosities reaching up to 150,000 mPa·s.
Detailed technical guidance for cosmetic brand buyers, quality control teams, and supply chain directors sourcing airless pump bottles from China manufacturers.
Threaded Airless Pumps feature screw-on necks allowing filling lines to easy screw caps on and off during trial runs, making them ideal for small-to-medium filling setups. However, threaded caps can technically be opened by consumers, compromising air isolation. Snap-On Airless Pumps utilize a permanent lock-ring design that snaps onto the bottle shoulder under pneumatic force. Once snapped, the container cannot be unsealed without destroying the bottle, guaranteeing maximum tamper-resistance, tamper-evidence, and zero oxygen leakage during consumer use.
At MYT Cosmetics, quality assurance begins with high-precision injection mold tooling crafted to tolerances within ±0.005mm. During production, automated optical sensors verify piston dimension accuracy. Random batch samples (AQL 0.65 Level II) undergo vacuum chamber leak testing at -0.08 MPa for 30 minutes in inverted positions, ensuring that expansion or pressure drops during air transport (flight cargo holds) will not induce pump leakage or seal degradation.
Our standard airless pump engines handle fluid viscosities from 500 cPs (liquid essences and light lotions) up to 60,000 cPs (heavy anti-wrinkle creams). For high-viscosity applications such as anhydrous ointments, oral toothpaste, and clay masks (up to 120,000 cPs), we supply specialized High-Viscosity Vacuum Pumps equipped with reinforced piston wiper seals, larger valve ports, and high-tensile external springs.
To satisfy stringent EU sustainability directives, we manufacture 100% Mono-Material Polypropylene (PP) airless systems where the actuator, pump stem, piston, and bottle cylinder are molded exclusively from PP resin. We eliminate all internal metal springs by substituting PP spring mechanisms or isolating the metal spring outside the product chamber. Additionally, we provide food-contact grade Post-Consumer Recycled (PCR-PP) resin options from 25% up to 100% inclusion rates.
Yes. Airless packaging is the industry standard for reactive formulas containing 15–20% L-Ascorbic Acid (Vitamin C), AHA/BHA chemical exfoliants, Retinoids, and active Peptide complexes. Because our non-metal liquid path designs prevent the formulation from touching metal components, metallic ion catalytic degradation is completely avoided. Furthermore, opaque or dual-wall frosted outer bodies can be specified to block UV radiation (190nm–400nm wavelengths) from breaking down light-sensitive active compounds.
We provide comprehensive surface decorating services including Pantone-matched custom color injection, matte soft-touch frosting, high-gloss UV lacquering, multi-color silk-screen printing, precision hot-foil stamping (gold, silver, rose gold, holographic), gradient spray painting, and custom electroplated metalized actuator rims.
Standard stocked catalog components have an MOQ of 3,000 to 5,000 units for immediate dispatch. Custom color injection and decorated private-label orders typically require an MOQ of 10,000 units per artwork SKU. Mass production lead time is generally 25 to 35 calendar days following pre-production sample approval and sign-off on artwork proofs.
Proper filling requires that the liquid bulk be dosed into the bottle cylinder from the top down, leaving minimal headspace (ideally under 3-5% of total volume) before inserting the pump assembly. When properly filled, the airless pump will prime and commence product flow within 2 to 4 initial strokes. We provide detailed filling height and volumetric clearance engineering specs for automated high-speed contract filling machinery.
100% PP mono-material airless bottles can be placed directly into standard curbside plastics recycling bins (RIC #5 Polypropylene). For multi-material acrylic outer designs, we offer easy-disassembly designs where the inner PP cartridge can be unclipped and separated from the PMMA outer shell for efficient sorting at municipal recycling plants.
We recommend conducting a 12-week accelerated stability test storing filled sample units at 45°C with 75% Relative Humidity (RH) alongside freeze-thaw thermal cycling (-10°C to 40°C). Key evaluations include measuring volumetric dosing consistency, verifying piston ascension smooth movement, inspecting for resin stress-cracking caused by formula essential oils, and monitoring active ingredient potency retaining curve over time.