Choosing among the 2026 Top GMP Certified Cosmetic Manufacturing Suppliers requires more than comparing glossy websites. A credible partner must show controlled production, trained personnel, traceable ingredients, and consistent batch records. GMP Certified Cosmetic Manufacturing is not simply a marketing phrase. It represents disciplined systems that protect product quality, consumer safety, and brand credibility.
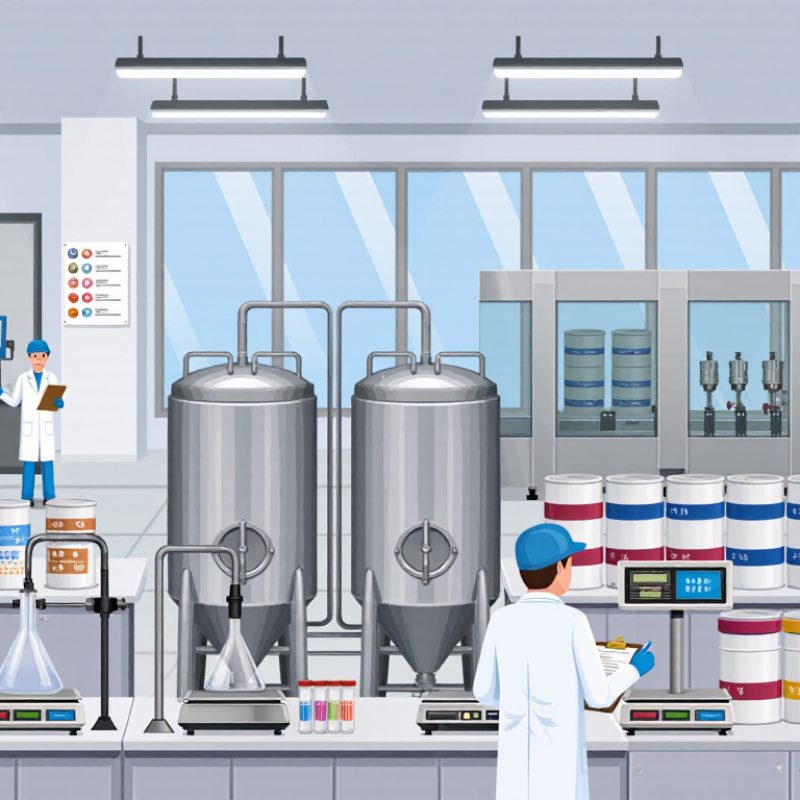
Quality-management authority W. Edwards Deming stated, “Quality comes not from inspection, but from the improvement of the production process.” This principle remains highly relevant to cosmetic manufacturing. A dependable supplier should demonstrate how it prevents errors before filling begins. Look for clearly labeled raw-material drums, calibrated weighing scales, documented cleaning procedures, and retained samples from every batch. These details reveal operational maturity.
This guide examines suppliers through practical evidence, including certification status, formulation capabilities, facility standards, testing procedures, minimum order quantities, and communication practices. It also considers whether manufacturers support stability testing, packaging compatibility, and regulatory documentation for different markets. A certificate alone cannot tell the whole story. Some suppliers present impressive credentials but provide limited technical transparency.
No manufacturer is flawless. Even experienced facilities may face delays, reformulation challenges, or communication gaps. Buyers should question claims, request current documentation, and verify production capabilities directly. Site audits and sample evaluations can expose weaknesses that brochures hide. The strongest GMP Certified Cosmetic Manufacturing partners combine compliance with responsive service, realistic timelines, and measurable quality controls. This comparison aims to support informed decisions, while recognizing that the best supplier depends on each brand’s formula, budget, market, and growth plans.
The 2026 GMP supplier landscape is shaped by three compliance expectations: ISO 22716, FDA requirements, and EU cosmetic rules. ISO 22716 focuses on controlled production, hygiene, documentation, storage, and quality release. It is a useful baseline, but certification alone does not prove consistent performance.
In the United States, FDA facility registration and product listing support regulatory readiness, yet they are not government approval seals. Suppliers should maintain traceable batch records, ingredient specifications, complaint files, and adverse-event procedures. In the EU, manufacturers must support a Product Information File, Cosmetic Product Safety Report, notification, and evidence of GMP conformity. EN ISO 22716 is widely used for that purpose. Data quality varies. A polished certificate may hide weak deviation control or incomplete supplier monitoring.
Tips: Ask for the certificate scope, audit date, issuing body, and covered site. Review recent batch records, microbial results, stability data, and recall procedures. Verify whether the factory or a subcontractor performs filling and testing. Keep written evidence.
From practical supplier reviews, small details often reveal maturity. Cleanroom entry logs should match production schedules. Label reconciliation should be easy to trace. I would also challenge unclear answers, even when the facility looks impressive. Compliance is not static. A supplier may meet ISO 22716 today, then struggle after rapid expansion, staff turnover, or equipment changes. That risk deserves documented follow-up.
Market-entry compliance checkpoints relevant to cosmetic manufacturing suppliers, based on publicly documented U.S. MoCRA and EU Cosmetics Regulation requirements.
The values represent the number of distinct compliance checkpoints shown in the selected framework, not a supplier ranking or certification score.
Sources: U.S. FDA Modernization of Cosmetics Regulation Act of 2022; Regulation (EC) No 1223/2009 on cosmetic products; ISO 22716:2007 Cosmetics — Good Manufacturing Practices.
2026 Top GMP Certified Cosmetic Manufacturing Suppliers?
GMP certification becomes meaningful when an auditor can trace every batch record. ISO 22716:2007 provides the practical framework for this review. It covers personnel, premises, equipment, production, quality control, storage, complaints, and recalls. A supplier should show controlled procedures, not simply display a certificate.
During an audit, inspectors may check training records beside a mixing room. They can compare cleaning logs with equipment labels and production dates. They may sample raw material records, weighing sheets, test results, and release approvals. Temperature logs should match storage requirements. Deviations should include investigation, corrective action, and documented approval. Supplier qualification also matters, especially for preservatives, fragrances, containers, and other critical materials.
Paperwork alone is not enough. A strong quality manager can explain why a procedure exists and how workers follow it. Operators should understand hygiene rules, protective clothing, line clearance, and contamination controls. I have found that small details often reveal process weakness. A missing signature may seem harmless, but repeated gaps can damage traceability. No audit is flawless. Even experienced teams may overlook an unclear instruction or an outdated form. That uncomfortable finding deserves attention, not concealment. When comparing 2026 suppliers, request recent audit findings, corrective-action evidence, batch traceability samples, and proof of ongoing staff training. Consistent records usually tell more than polished marketing language.
| No. | Supplier Evaluation Dimension | ISO 22716:2007 Audit Expectation | Objective Evidence to Request | Suggested Evaluation Weight | Priority |
|---|---|---|---|---|---|
| 1 | GMP Scope and Certification Status | The site should demonstrate cosmetic GMP conformity. ISO 22716:2007 is a GMP guideline and does not itself issue a universal certificate; certification or audit recognition depends on the independent certification body or customer program. | Current certificate or audit report, certification scope, covered site address, product categories, issue date, expiry date, and certification-body details. | 12% | Critical |
| 2 | Quality Management System | Documented quality responsibilities, controlled procedures, batch-release controls, deviation management, corrective and preventive actions, and management review should be established. | Quality manual or system overview, organization chart, approved procedures, training records, deviation and CAPA summaries, and management-review records. | 12% | Critical |
| 3 | Personnel Competence and Hygiene | Personnel should be suitably qualified, trained for assigned duties, and protected against practices that could contaminate products or materials. | Job descriptions, GMP training matrix, training effectiveness checks, health and hygiene procedures, gowning rules, and visitor-control records. | 7% | High |
| 4 | Premises, Zoning and Material Flow | Facilities should support orderly operations, prevent mix-ups and contamination, and provide suitable areas for receipt, storage, production, packaging, laboratory work, and finished goods. | Facility layout, personnel and material-flow diagrams, cleaning records, pest-control records, environmental monitoring where applicable, and maintenance logs. | 9% | High |
| 5 | Equipment Qualification and Maintenance | Equipment should be suitable for intended use, cleanable, maintained, calibrated or checked when necessary, and protected from contamination. | Equipment inventory, preventive-maintenance schedule, calibration certificates, cleaning validation or verification records, and equipment-use logs. | 8% | High |
| 6 | Raw Material and Packaging Control | Materials should be purchased from approved sources, received against defined requirements, identified by status, sampled or tested as appropriate, and released before use. | Approved-supplier list, specifications, certificates of analysis, incoming inspection records, quarantine and release labels, sampling procedures, and traceability records. | 10% | Critical |
| 7 | Production and In-Process Controls | Manufacturing should follow approved instructions with defined controls for weighing, mixing, processing parameters, yield, bulk identification, and prevention of cross-contamination. | Master manufacturing instructions, batch records, line-clearance checklists, weighing verification, in-process test results, yield reconciliation, and operator sign-offs. | 12% | Critical |
| 8 | Quality Control Laboratory | Testing and inspection activities should use approved methods, suitable equipment, qualified personnel, and documented results supporting material and product decisions. | Specifications, test methods, method-verification records where applicable, analyst training, reference-standard controls, laboratory worksheets, and retained-sample procedures. | 9% | High |
| 9 | Finished Product Release | Finished products should be assessed against approved specifications and formally released by authorized quality personnel before distribution. | Finished-product specifications, release checklist, batch disposition records, microbiological results where applicable, and quality-authorized release signatures. | 8% | Critical |
| 10 | Documentation and Data Integrity | Documents and records should be legible, approved, traceable, protected from unauthorized changes, retained for defined periods, and readily retrievable. | Document-control procedure, revision history, electronic-system access controls, audit trails where applicable, record-retention schedule, and sample completed records. | 8% | Critical |
| 11 | Complaints, Recalls and Traceability | The supplier should investigate complaints, assess product risk, maintain distribution traceability, and operate a documented recall process when necessary. | Complaint procedure, complaint register, investigation reports, mock-recall results, distribution records, recall decision tree, and regulatory-notification process. | 7% | High |
| 12 | Change Control, Deviations and CAPA | Planned changes and unexpected deviations should be documented, risk-assessed, approved, investigated, and followed by effective corrective or preventive actions where required. | Change-control log, deviation investigations, root-cause analysis, CAPA effectiveness checks, impact assessments, and customer-notification records. | 8% | Critical |
| 13 | Subcontracting and Supply-Chain Oversight | Outsourced activities should be clearly defined, controlled by written agreements, performed by qualified parties, and subject to appropriate quality oversight. | Technical or quality agreements, subcontractor qualification records, audit reports, responsibility matrix, approved subcontractor list, and subcontractor performance reviews. | 5% | High |
| Total suggested supplier-assessment weighting | 115% | Normalize to 100% | |||
In 2026, GMP certification is only the starting filter for cosmetic manufacturing suppliers.
I compare the certificate’s scope, issuing body, expiry date, and covered production lines. A certificate without current audit evidence deserves caution. Ask for recent batch records, deviation summaries, CAPA responses, certificates of analysis, microbial results, and stability data. Quality claims should be traceable to actual batches.
MOQ affects cash flow and testing risk.
Confirm whether the quoted MOQ applies to one formula, one scent, or each package size. Also check pilot quantities before commercial production. Lead time needs careful definition. It may include raw material purchasing, filling, laboratory testing, and final release. A supplier promising 30 days may mean 30 days after all materials arrive. Get every stage written down.
Capacity is more than monthly output.
Review line speed, filling formats, staffing, maintenance schedules, and peak-season availability. Request a production plan for your expected volume. I prefer suppliers that explain constraints clearly. That feels more reliable.
A weighted comparison sheet can score MOQ, lead time, capacity, documentation, and quality performance separately.
My own mistake was trusting a polished presentation before checking release timelines. The factory looked capable, but testing created delays. Ask for practical evidence, not perfect language. Small gaps may be manageable; unexplained gaps are different.
A credible supplier ranking should begin with verified GMP certification, not polished sales claims. Check the certificate issuer, covered facility, product scope, and expiration date. An audit report should match the factory address. That detail matters. During supplier reviews, I also examine batch records, sanitation logs, training files, and environmental monitoring results. A clean production room means little without consistent documentation.
Recall records deserve careful reading. One recall may reflect a strong reporting system, while repeated recalls can indicate weak root-cause controls. Compare recall frequency, affected batches, response time, and corrective actions over several years. Defect metrics add another layer. Useful figures include rejected batches, customer complaints, fill-weight variation, microbial failures, and out-of-specification results. However, reported rates are not always comparable. Some factories count minor packaging marks; others do not. That limitation should remain visible in any ranking.
Tips: Request twelve months of anonymized quality data and three recent corrective-action reports. Ask how defects are sampled and calculated. Visit the facility if practical, and observe line clearance, label control, and retained-sample storage. Do not accept “zero defects” without evidence. Even reliable manufacturers make mistakes. What matters is whether they detect problems early, investigate honestly, and prevent recurrence. A supplier with transparent weaknesses may be safer than one presenting perfect but unsupported numbers.
A GMP claim deserves evidence, not a polished badge. The FDA does not “certify” cosmetic manufacturing facilities. Under MoCRA, facilities must register with the FDA, renew registration biennially, and report serious adverse events within 15 business days. Ask for the FDA registration record, but do not treat registration as GMP approval. Check the facility’s ISO 22716 certificate, including its exact site, product scope, issue date, expiry date, and certification body. Verify that body through its accreditation directory. The ISO Survey 2023 recorded 1,265,216 ISO 9001 certificates worldwide, yet ISO 9001 alone does not prove cosmetic GMP compliance.
Look closer. Request recent audit findings, corrective-action records, batch manufacturing records, cleaning logs, water-test results, and supplier-traceability documents. A credible facility should show how it handles deviations, rejected materials, complaints, and mock recalls. In the EU, confirm alignment with Regulation (EC) No. 1223/2009, including a Product Information File, Cosmetic Product Safety Report, and designated Responsible Person. The European Commission’s Safety Gate 2023 report identified cosmetics as 32% of reported dangerous-product alerts. That figure makes document review more than paperwork. It is a risk screen. Still, documents can be incomplete, outdated, or carefully selected. I would compare certificates against a live production tour and one anonymized batch file. That extra step may feel excessive. It is often the missing one.
Check the certificate’s scope, issuing body, expiry date, and covered production lines. Not just badges. Request recent audit findings, batch records, cleaning logs, and corrective-action records. A certificate without current evidence deserves caution.
No. Registration shows administrative status, not complete manufacturing compliance. In the United States, facilities must renew registration every two years. Serious adverse events must be reported within 15 business days. Verify registration separately from GMP certification.
Ask for certificates of analysis, microbial results, stability data, and supplier-traceability records. Review rejected-material logs and complaint handling. Request one anonymized batch file. Quality claims should connect to actual production batches.
Confirm whether the MOQ applies to each formula, scent, package size, or total order. Ask about pilot quantities before commercial production. A smaller pilot can reduce cash-flow pressure and testing risk. I once treated one quoted MOQ as universal. That assumption was wrong.
Define every stage in writing. Include raw material purchasing, filling, laboratory testing, and final release. A “30-day” promise may begin after all materials arrive. Ask for separate dates, not one attractive total.
Review line speed, filling formats, staffing, maintenance schedules, and peak-season availability. Request a production plan for your expected volume. Monthly output alone is incomplete. Clear limitations often feel more trustworthy.
Some markets require a product information file, a safety report, and a designated responsible person. Confirm the exact requirements for your sales region. Keep formula, testing, and batch records consistent. Missing documents can delay release.
Score MOQ, lead time, capacity, documentation, and quality performance separately. Add evidence links beside each score. Compare promised timelines with actual release records. Polished presentations can hide laboratory delays. Small gaps may be manageable; unexplained gaps are different.
This guide presents a practical 2026 overview of the GMP Certified Cosmetic Manufacturing supplier landscape, focusing on ISO 22716:2007, FDA expectations, and EU compliance documentation. It explains how GMP certification is evaluated through audit requirements covering hygiene, personnel training, raw material control, production processes, packaging, storage, traceability, and corrective actions. Readers will learn how to distinguish verified compliance from unsupported marketing claims by reviewing current certificates, audit records, registration information, and relevant quality documents.
The article also offers a structured method for comparing suppliers according to minimum order quantities, lead times, production capacity, testing resources, quality systems, recall history, and defect-rate data. A supplier ranking framework is introduced to help buyers assess transparency, certification validity, operational reliability, and risk-management performance. By using documentation from recognized regulatory and standards organizations, businesses can make informed decisions and select manufacturing partners that support consistent product quality, responsible production, and long-term compliance.